Explore our elite class of medical instruments, surgical devices, and advanced sterile infrastructure designed to empower healthcare providers globally.
Built upon two decades of precision engineering, strict quality compliance, and unyielding dedication to human healthcare advancement.
Established in May of 2004, Nanjing Seeker Medical Co., Ltd. is a professional manufacturer specialized in research, development, production of surgical sutures and surgical needles. All of our products comply with international and interior quality standards, and are approved Production license, CE, ISO13485, ISO14001, ISO45001 certificates.
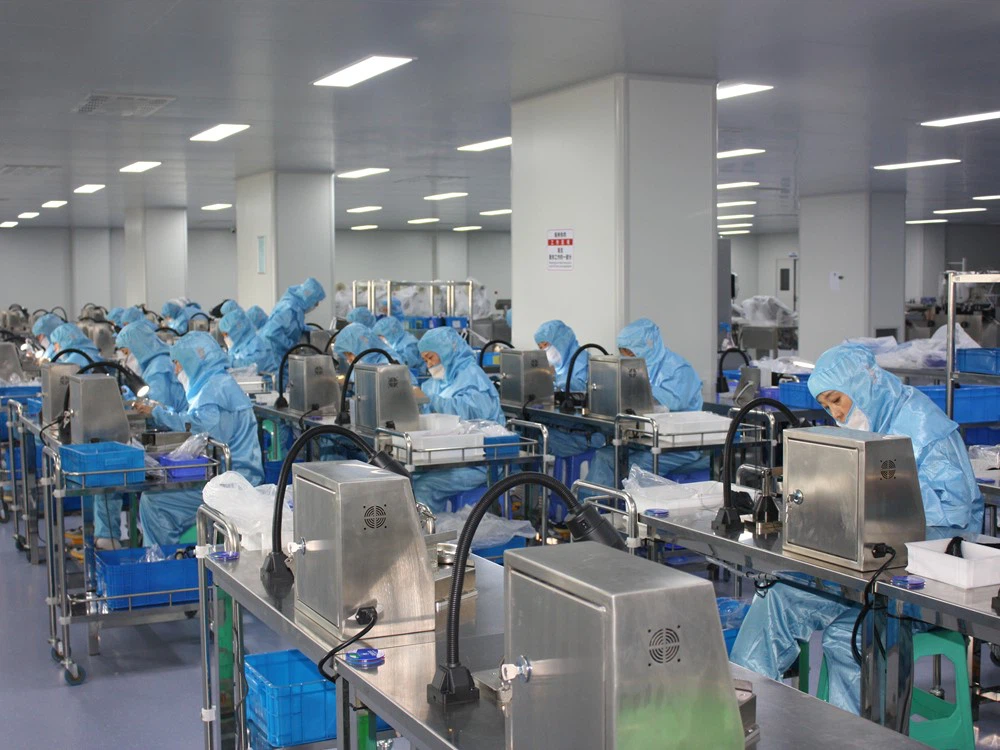
We insist on the quality policy of modern techniques, excellent quality, customers satisfaction. We attach great importance to the development and application of new technology, so far, we have obtained 29 new invention patents, we have realized the automatic transformation of the production process. And we are greatly appreciated in variety of different markets throughout the world.
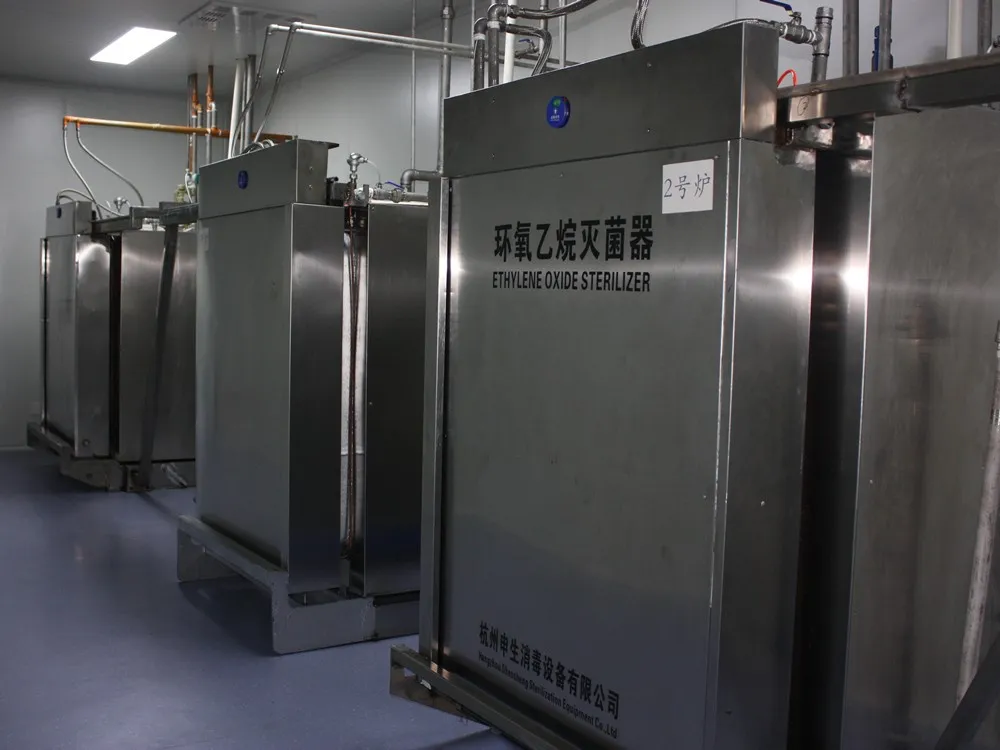
All staffs in our company welcome every friend from home and abroad. Let us make more efforts for human health career.
Navigating the next generation of medical device integrity through smart material science and automated barrier technologies.
Integrating nanotechnology and eco-friendly polymers to deliver ultra-low microbial penetration while maintaining breathability for EtO and gamma sterilization modalities.
Developing embedded colorimetric and digital indicators that track temperature excursions, humidity shifts, and package seal breaches throughout transit.
Transitioning toward recyclable medical-grade substrates that lower carbon footprints without compromising ISO 11607 sterilization validation benchmarks.
Comprehensive packaging paradigms engineered for diverse clinical workflows, surgical suites, and pharmaceutical laboratories.
Tailored sterile pouches and peel-open blister packs designed for rapid aseptic presentation of precision surgical instruments and sutures.
Heavy-duty multi-layer barrier bags resistant to puncture and abrasion, ensuring absolute sterility for metallic and ceramic implants.
Customized compartmentalized trays maintaining dual-chamber isolation for rapid testing reagents and sterile collection consumables.
Individual hermetic sealing solutions guaranteeing zero moisture ingress for advanced self-adhesive dressings and surgical gauzes.
Navigating complex international regulatory landscapes with verified quality management systems and dedicated regional support.
Fully compliant with CE, ISO 13485, ISO 14001, and ISO 45001, ensuring complete traceability from raw material to final delivery.
Providing comprehensive validation dossiers, biocompatibility testing reports, and sterilization certificates to accelerate local market clearance.
Our multilingual engineering team offers personalized consultation regarding packaging validation, shelf-life testing, and custom OEM/ODM specifications.
Leveraging state-of-the-art automation and intelligent manufacturing to deliver unmatched cost efficiency and scalable output.
ISO Class 7 and Class 8 controlled manufacturing environments equipped with robotic sealing and automated optical inspection (AOI) systems.
Advanced ERP-driven supply chain management guaranteeing continuous raw material availability and mitigated geopolitical or logistical risks.
High-speed production lines capable of fulfilling large-scale multinational enterprise orders with stringent delivery timelines.
Advanced manufacturing efficiencies passing direct cost-benefits to global partners while maintaining uncompromising premium quality.
Addressing the core criteria demanded by world-class medical distributors, hospital networks, and pharmaceutical giants.
Flexible manufacturing capabilities to customize dimensions, print branding, and barrier specifications according to unique institutional requirements.
Strict multi-stage inspection protocols covering seal integrity, burst pressure testing, and microbial barrier verification before shipment.
Strategic partnerships with premier global freight forwarders ensuring secure, temperature-controlled, and timely door-to-door delivery.
Discover additional specialized medical consumables and surgical accessories crafted under rigorous factory standards.
Expert insights addressing common technical and procurement inquiries regarding our sterile packaging and surgical product solutions.
All our manufacturing processes and products strictly comply with international standards. We hold official production licenses alongside CE, ISO 13485 (medical devices quality management), ISO 14001 (environmental management), and ISO 45001 (occupational health and safety) certifications.
We utilize advanced multi-layer medical-grade polymers and breathable webs designed to withstand pressure differentials, moisture, and puncture risks. Every batch undergoes rigorous seal strength and burst testing in compliance with ISO 11607 validation protocols.
Yes. With over 29 invention patents and fully automated production lines, we provide customized dimensions, branding, specialized barrier coatings, and tailored packaging configurations to meet the specific requirements of global medical device companies.
Thanks to our Industry 4.0 automated factory transformation and robust raw material inventory buffers, we maintain high production capacity and efficient scheduling, ensuring timely delivery for worldwide distributors and hospital groups.
 Seeker Medical